LabTech MVP-12 Automatic Parallel Vacuum Concentrator
Part Number: US-MVP12
Couldn't load pickup availability
Overview
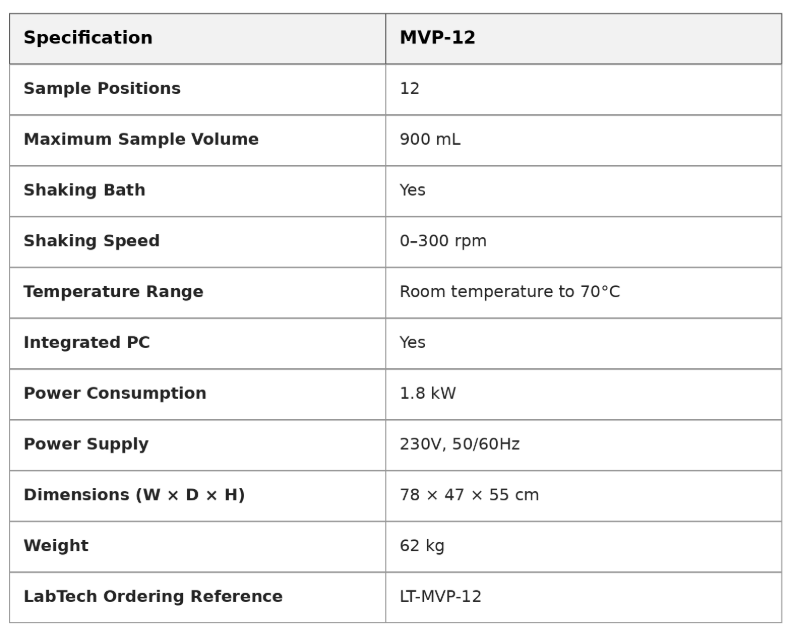
The LabTech MVP-12 Automatic Parallel Vacuum Concentrator is designed for high-throughput concentration of large-volume laboratory samples. The system can process up to 12 samples simultaneously, with sample volumes up to 900 mL each, making it particularly suitable for extraction and concentration workflows requiring greater sample capacity.
Vacuum concentration lowers the boiling point of solvents, enabling efficient evaporation at reduced temperatures and helping protect heat-sensitive sample components. The MVP-12 combines vacuum, controlled heating, and shaking to automate the concentration process while improving laboratory throughput and reducing the need for multiple individual evaporation systems. LabTech states that a single MVP-12 can replace up to 12 rotary evaporators in suitable workflows.
Key Features
12-position parallel vacuum concentration
Supports sample volumes up to 900 mL per position
Designed for large-volume and high-throughput applications
Fully surrounded water-bath heating for efficient heat transfer
0–300 rpm shaking range
Temperature control from room temperature to 70°C
Independent airflow pathways help prevent cross-contamination and backflow between samples
Integrated computer control
Heated upper cover helps reduce condensation
Safety-lock cover design for secure and convenient operation
High solvent recovery capability
Compact integrated system design
Vacuum Concentration
The MVP-12 reduces pressure within the concentration system, lowering the boiling point of the solvent. This allows evaporation to occur at lower temperatures than under atmospheric conditions.
Combined with controlled water-bath heating and sample agitation, the system provides efficient concentration while helping protect thermally sensitive sample components. Recovered solvent vapor can also be collected rather than being released directly into the laboratory environment.
Applications
The MVP series is designed for sample preparation across applications including:
- Environmental analysis
- Food and agricultural testing
- Pharmaceutical analysis
- Chemical laboratories
- Extraction workflows
- Natural product samples
- Heat-sensitive sample preparation
- Solvent evaporation and sample volume reduction
Technical Specifications

System Design
The current MVP series uses a compact, self-contained design in which the vacuum module integrates the pump, condenser, waste bottle and controller, reducing the overall footprint and simplifying system maintenance. LabTech redesigned the MVP family in 2026 around this more integrated architecture.
Compatible Temperature Control
LabTech specifically promotes the MVP Vacuum Concentrator + LabTech Water Chiller as an all-in-one evaporation package designed for high solvent recovery and throughput.